Introduction
Mild steel pipe, fundamentally composed of carbon steel with a low carbon content (typically 0.05% to 0.25%), occupies a critical position within the global infrastructure and industrial sectors. Its prevalence stems from a favorable combination of cost-effectiveness, weldability, machinability, and adequate strength for numerous applications. Within the industry chain, mild steel pipe serves as a crucial intermediary product, connecting steel mills to downstream industries encompassing construction, oil and gas, water conveyance, and manufacturing. Understanding its pricing dynamics, performance characteristics, and potential failure modes is paramount for effective procurement, engineering design, and long-term operational sustainability. Core performance indicators include yield strength, tensile strength, dimensional accuracy, corrosion resistance (influenced by surface treatment), and conformity to relevant industry standards. Fluctuations in iron ore prices, energy costs, and global supply chain disruptions significantly influence mild steel pipe pricing, creating challenges for budgetary control and project feasibility.
Material Science & Manufacturing
Mild steel’s defining characteristic is its relatively low carbon content, which imparts ductility and weldability. The primary raw material is iron ore, refined through processes like the Basic Oxygen Furnace (BOF) or Electric Arc Furnace (EAF) to produce molten steel. Alloying elements, such as manganese (typically 0.7-0.9%), silicon (0.15-0.3%), and phosphorus (maximum 0.04%), are added to refine grain structure and enhance mechanical properties. The manufacturing of mild steel pipes commonly employs several methods: seam welding (Electric Resistance Welding - ERW, Submerged Arc Welding - SAW), and seamless extrusion. ERW pipes are produced by forming steel strips into a cylindrical shape and welding the seam using electric current. SAW pipes utilize a submerged arc welding process for thicker walls and larger diameters. Seamless pipes are manufactured by piercing a solid billet of steel and subsequently drawing or rolling it to the desired dimensions. Critical parameter control during manufacturing includes maintaining precise chemical composition, consistent wall thickness, adequate weld penetration (for welded pipes), and dimensional tolerances verified through non-destructive testing (NDT) techniques like ultrasonic testing and radiographic inspection. Heat treatment processes, such as normalizing or annealing, are employed to relieve residual stresses and improve the steel’s microstructure.
Performance & Engineering
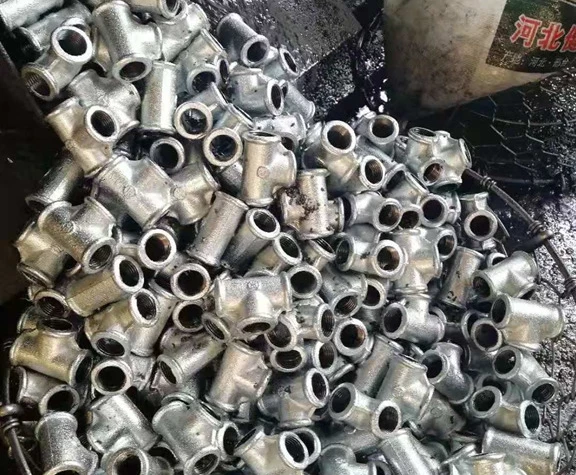
The performance of mild steel pipe is dictated by its mechanical properties and environmental resistance. Force analysis, especially when subjected to internal pressure, requires considering the hoop stress (σh = PD/2t, where P is pressure, D is diameter, and t is wall thickness) and longitudinal stress (σl = PD/4t). These stresses must remain below the material’s yield strength to prevent permanent deformation. Corrosion is a significant concern; mild steel is susceptible to oxidation in humid environments, leading to rust formation. Protective measures include applying coatings (e.g., epoxy, polyurethane, galvanization) or utilizing sacrificial anodes (cathodic protection). Engineering design must also account for thermal expansion/contraction, particularly in high-temperature applications, to prevent stress concentrations and potential cracking. Relevant compliance requirements include adherence to ASME B31.3 for process piping, API 5L for line pipe (oil and gas transportation), and EN 10208-2 for seamless steel tubes. Load bearing capacity, ductility, and impact resistance are further critical parameters, depending on the application, specifically in structural uses where cyclic loading and seismic activity must be considered. Fatigue analysis is often conducted to predict the lifespan of pipes subjected to repeated stress cycles.
Technical Specifications
| Parameter | Unit | ASTM A53 Grade B | API 5L X42 |
|---|---|---|---|
| Yield Strength | MPa | 250 | 345 |
| Tensile Strength | MPa | 400 | 485 |
| Elongation | % | 22 | 20 |
| Wall Thickness | mm | 2-25 | 3.2-25.4 |
| Outside Diameter | mm | 10-660 | 21.3-1219 |
| Carbon Content (max) | % | 0.25 | 0.24 |
Failure Mode & Maintenance
Mild steel pipes are susceptible to several failure modes. Corrosion, as previously mentioned, is a primary concern, leading to pitting, general thinning, and eventual perforation. Fatigue cracking can occur under cyclic loading, initiating at stress concentrators (e.g., welds, dents). Hydrogen embrittlement, prevalent in sour gas environments, can reduce ductility and cause brittle fracture. Erosion, caused by the impact of abrasive particles in fluids, can wear away the pipe wall. Creep, a time-dependent deformation under sustained stress at elevated temperatures, can occur in high-temperature applications. Maintenance strategies include regular inspection using NDT methods (visual inspection, ultrasonic testing, radiographic testing, eddy current testing), application of protective coatings, cathodic protection, and implementation of a robust corrosion monitoring program. For welded pipes, periodic weld inspections are crucial to detect cracks or defects. Repair methods include welding (for minor defects) or pipe replacement (for extensive damage). Preventive maintenance, such as proper insulation and drainage, can mitigate corrosion and other forms of degradation.
Industry FAQ
Q: What is the impact of varying sulfur content on the weldability of mild steel pipe?
A: Increased sulfur content in mild steel negatively impacts weldability. Sulfur forms iron sulfide (FeS) at grain boundaries, which lowers the melting temperature and creates hot cracking susceptibility during welding. Lower sulfur content grades (typically below 0.02%) are preferred for critical welded applications. Controlled cooling rates post-weld are also essential to minimize the risk of sulfide formation.
Q: How do different coating types (epoxy vs. polyurethane vs. galvanization) compare in terms of corrosion protection for mild steel pipe?
A: Galvanization provides sacrificial protection; the zinc coating corrodes preferentially, protecting the steel. It's cost-effective but offers limited abrasion resistance. Epoxy coatings offer excellent adhesion and chemical resistance but are susceptible to UV degradation. Polyurethane coatings combine good chemical resistance with improved UV resistance and abrasion resistance, making them a premium option. The choice depends on the specific environment and service conditions.
Q: What is the significance of Charpy V-notch impact testing, and at what temperatures is it typically performed for mild steel pipe intended for cold-weather applications?
A: Charpy V-notch impact testing measures a material's toughness – its ability to absorb energy and resist brittle fracture. For cold-weather applications, testing is typically performed at increasingly lower temperatures (e.g., -20°C, -40°C, -60°C) to determine the ductile-to-brittle transition temperature (DBTT). The pipe material must exhibit adequate impact resistance even at the lowest anticipated operating temperature.
Q: What are the key differences between ASTM A53 and API 5L specifications for mild steel pipe, and when would you specify one over the other?
A: ASTM A53 covers a broader range of pipe applications, including structural and pressure applications, and allows for both welded and seamless construction. API 5L is specifically designed for line pipe used in the oil and gas industry, with stricter requirements for toughness, weld quality, and hydrostatic testing. API 5L is chosen for high-pressure, long-distance pipelines, while ASTM A53 is suitable for less demanding applications.
Q: How does the manufacturing process (ERW, SAW, Seamless) influence the cost and mechanical properties of mild steel pipe?
A: ERW is generally the most cost-effective method, suitable for smaller diameters and thinner walls. SAW offers higher strength and thicker walls at a moderate cost. Seamless pipe is the most expensive due to the complex manufacturing process, but it offers superior strength, uniformity, and is preferred for critical high-pressure applications where weld defects are a concern.
Conclusion
Mild steel pipe remains a cornerstone material in numerous industries due to its balance of cost, performance, and manufacturability. A thorough understanding of its material science, manufacturing processes, and potential failure modes is crucial for optimizing its application and ensuring long-term reliability. Precise control of chemical composition, rigorous quality control during manufacturing, and the implementation of effective corrosion protection strategies are essential for maximizing its lifespan and minimizing the risk of costly failures.
Future trends will likely focus on the development of higher-strength, more corrosion-resistant mild steel alloys, and advanced coating technologies. Furthermore, increasing emphasis on sustainable practices will drive the adoption of recycled materials and energy-efficient manufacturing processes. The effective utilization of digital technologies, such as predictive maintenance and real-time corrosion monitoring, will further enhance the operational efficiency and safety of mild steel pipe systems.
